Why choose T2
1
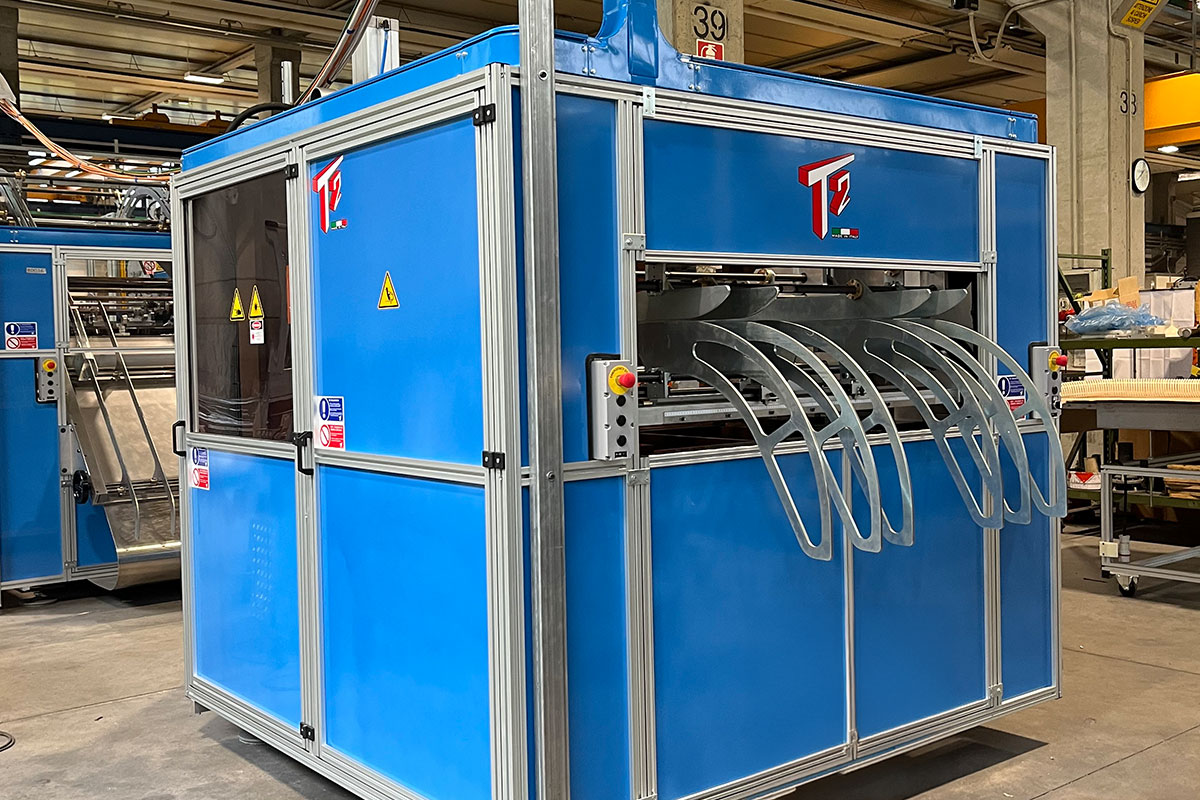
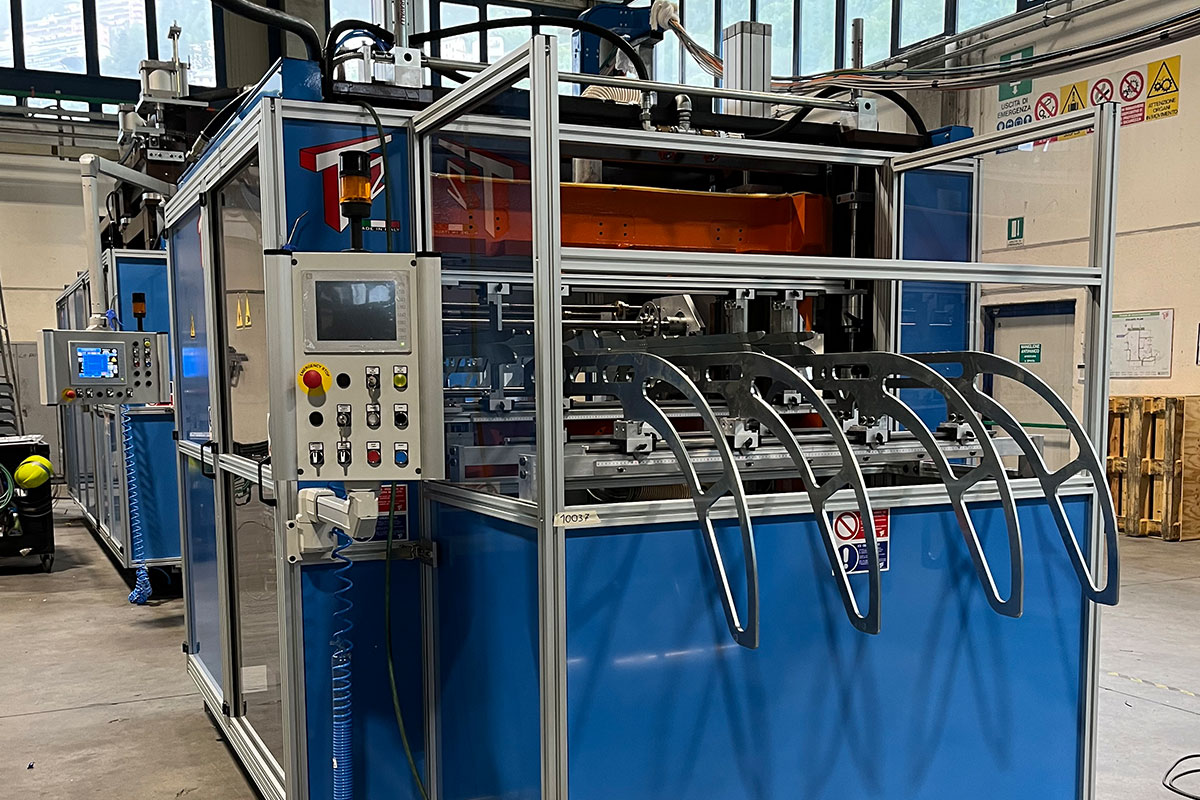
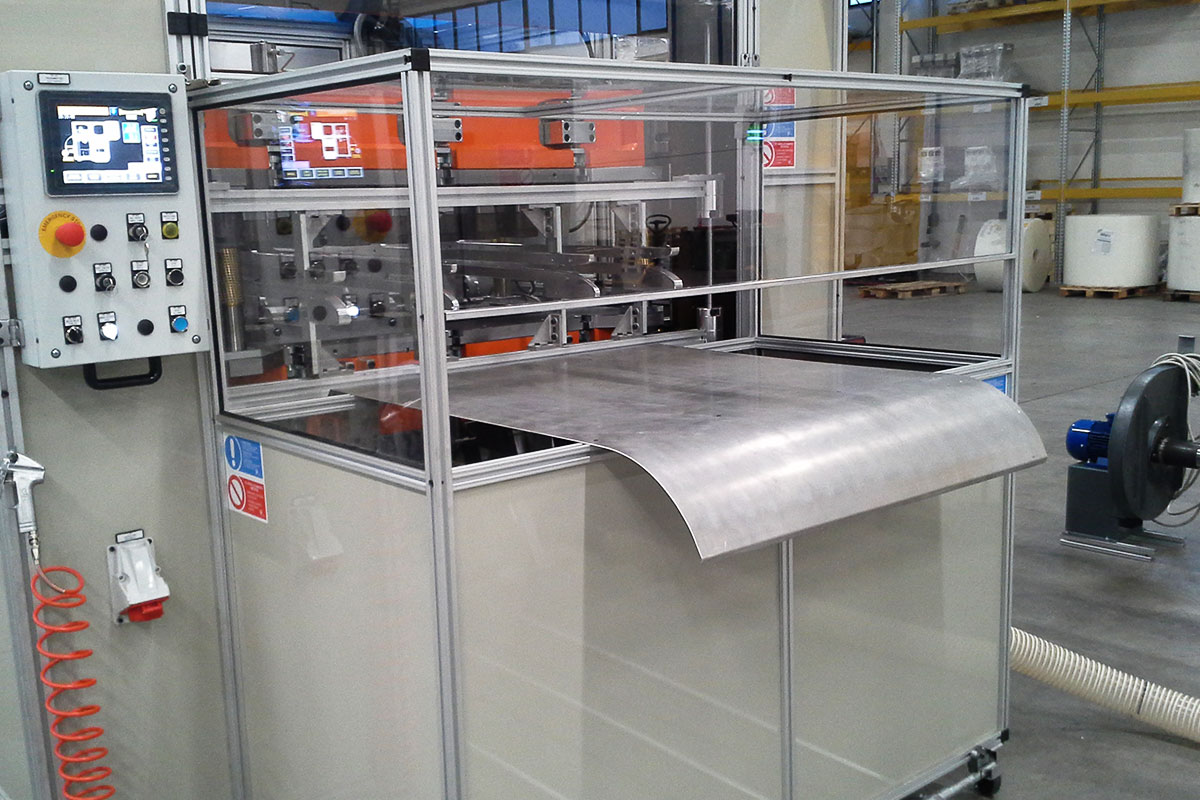
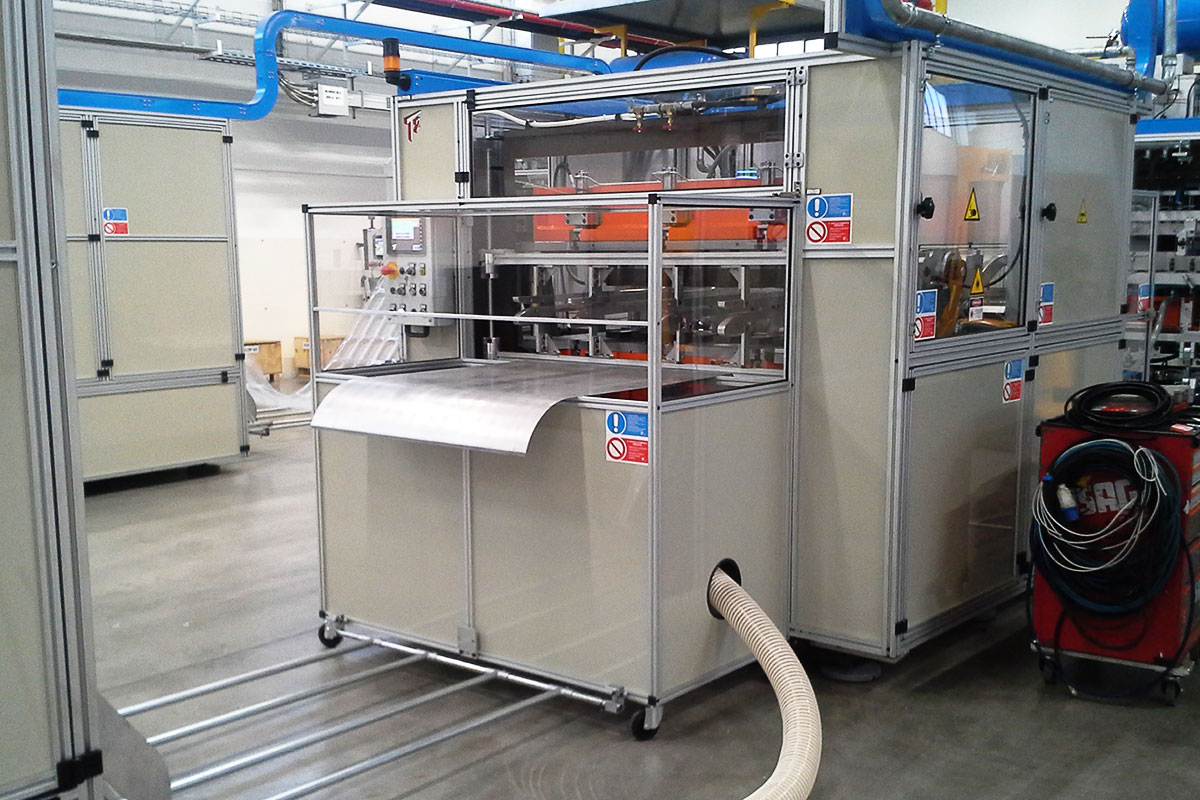
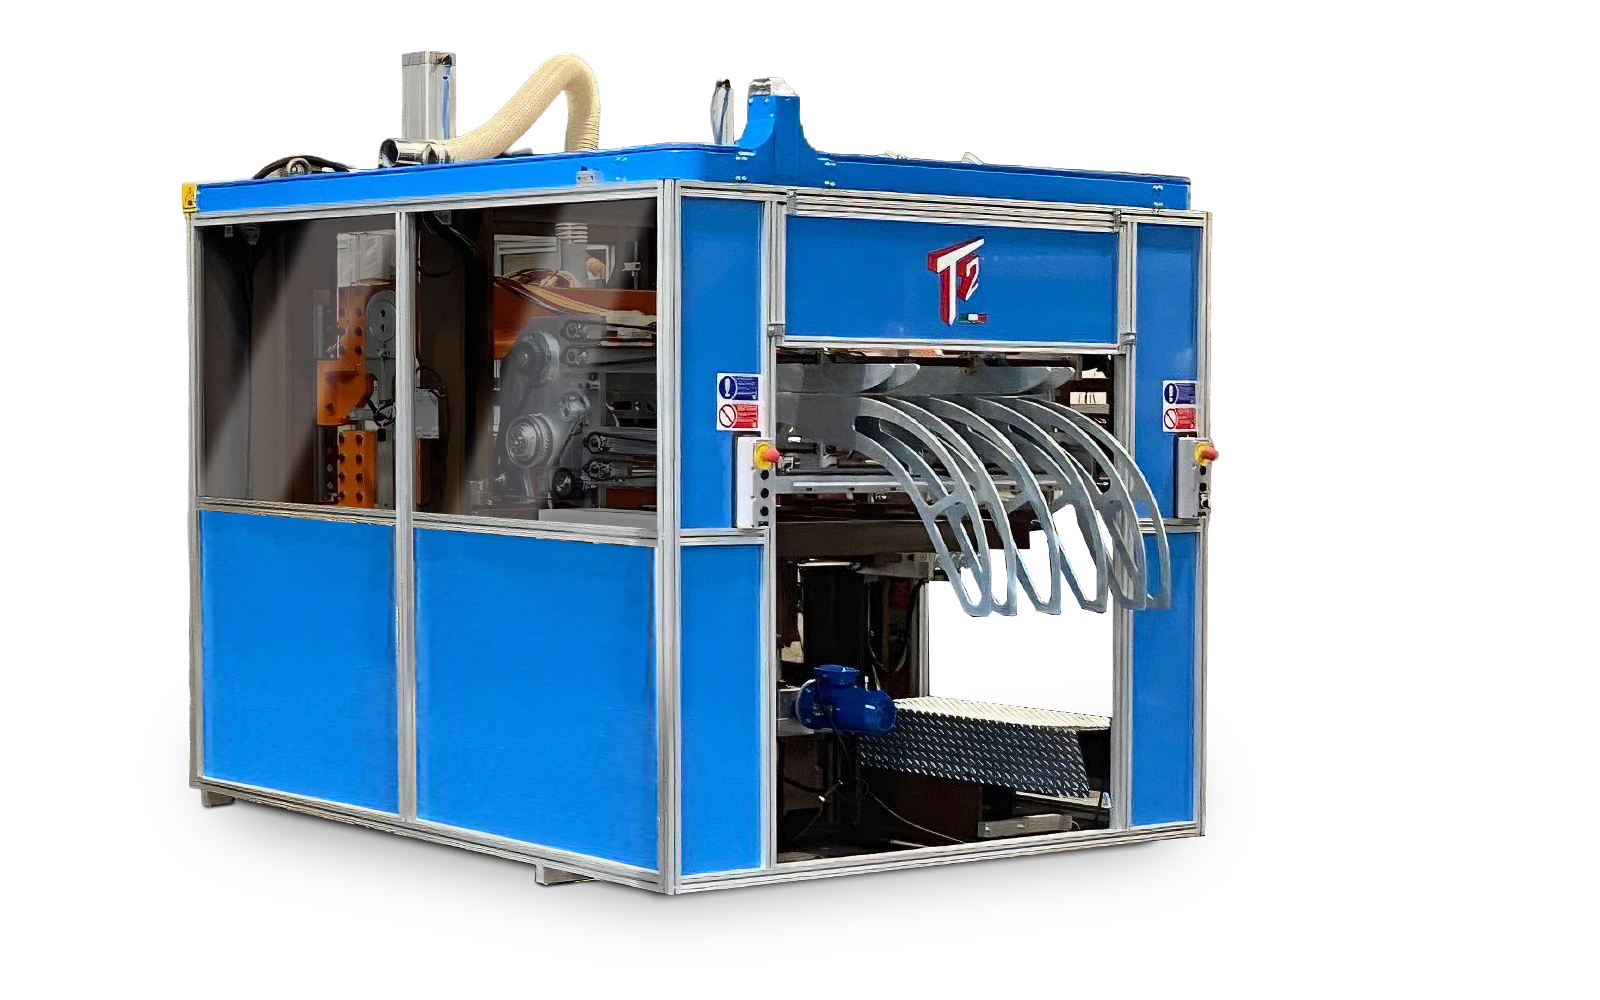
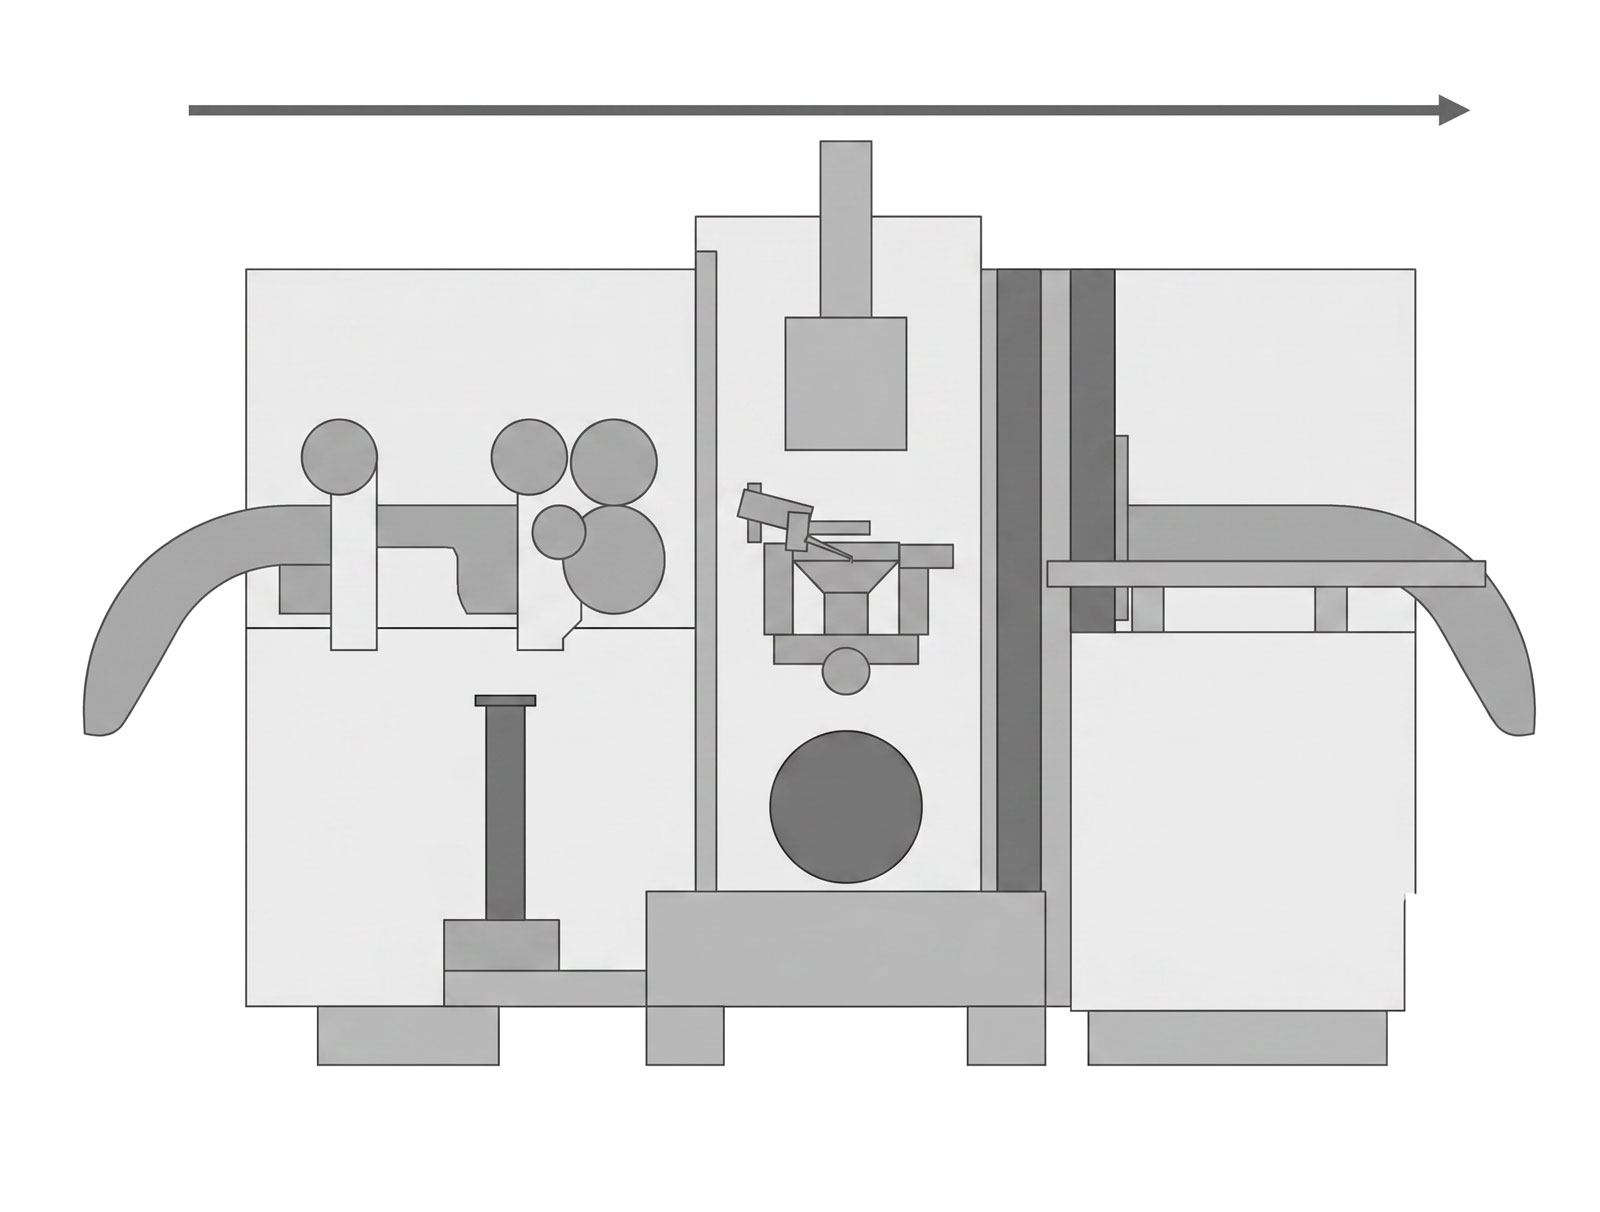
Simultaneous punching of multiple cavities to maximize cycle productivity
2
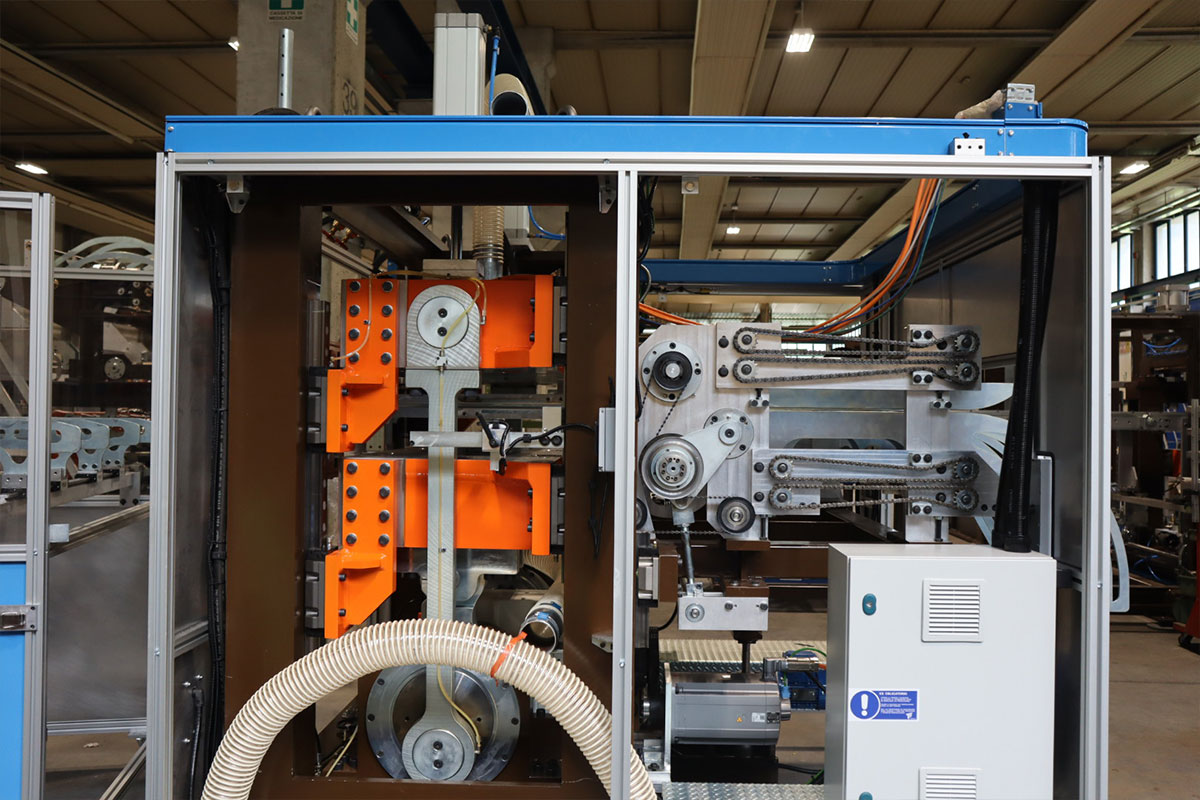
Integrated photocell for automatic and precise adjustment of the sheet pitch
3
Dedicated extraction system for continuous removal of punching waste
4
High operating speed
Technical specification
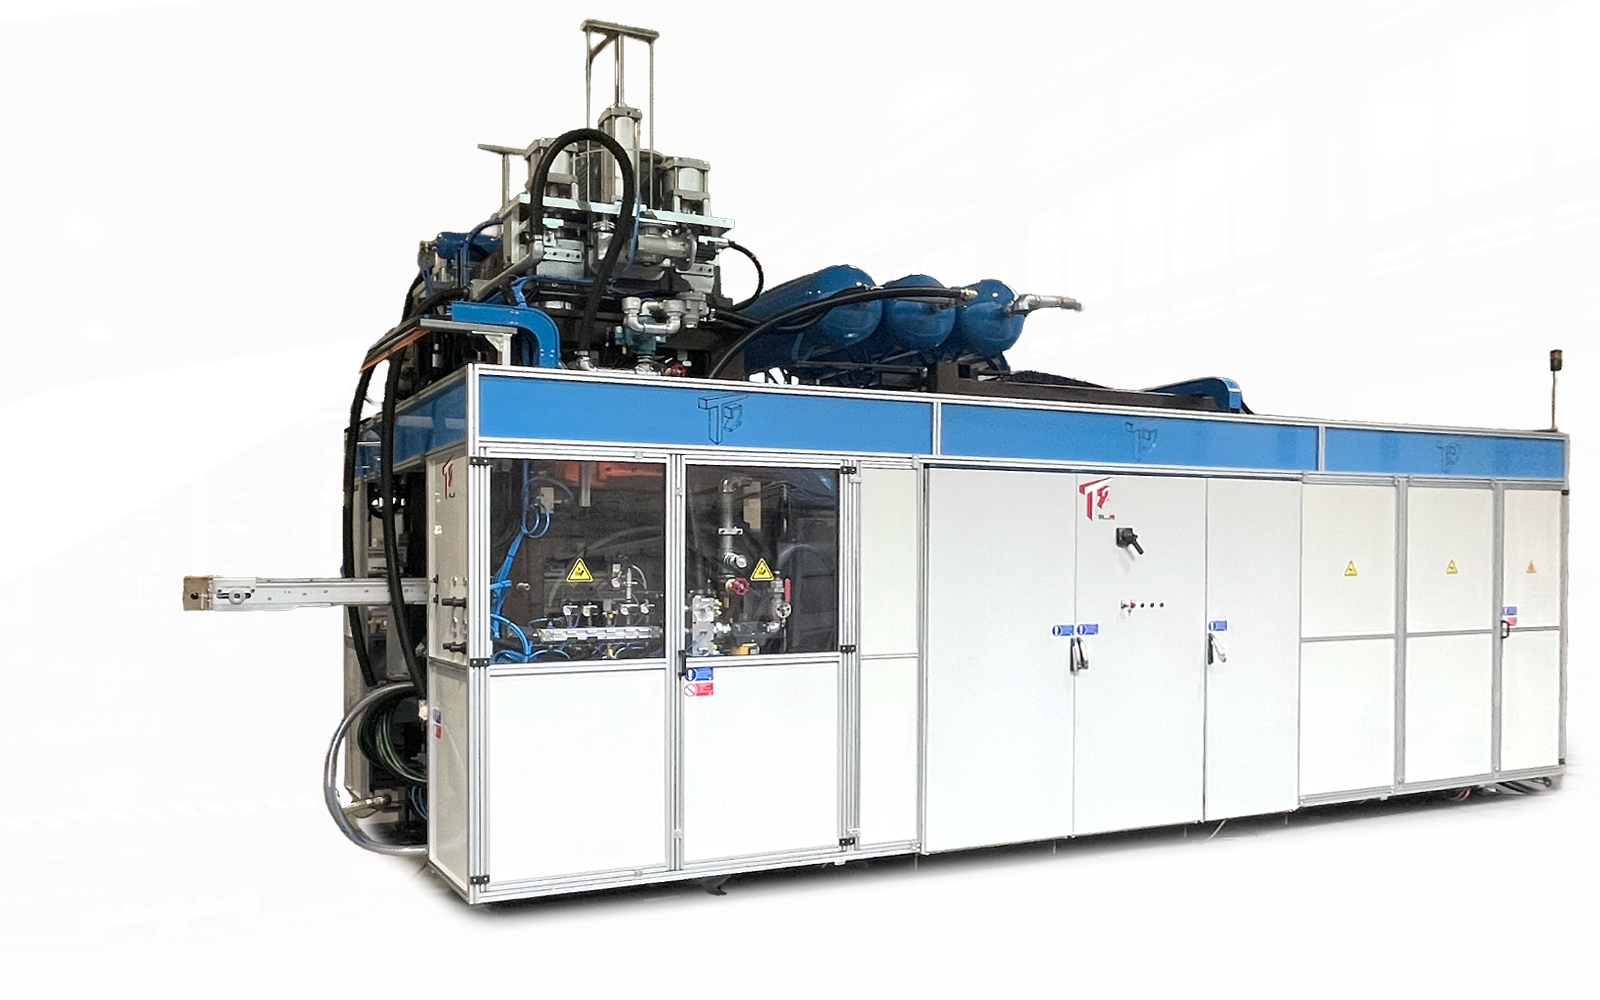
| Dimensions (width × length × height), mm | 2600 × 3750 × 2750 | ||
| Weight (approx.), kg | 10500 | ||
| Power consumption, kW | 15 | ||
| Maximum speed, rpm | 100 | ||
| Maximum punching depth, mm | 120 | ||
| Maximum sheet width, mm | 1400 | ||
| Maximum mould dimensions, mm | 15000 | ||
| Maximum punching area, mm | 1560 × 850 | ||
| Clearance between closed platens, mm | 250 | ||
| Upper moving platen stroke, mm | 150 | ||
| Lower moving platen stroke, mm | 50 | ||
| Platen closing adjustment, mm | ±5 | ||
| Maximum platen closing force, daN | 15000 | ||
| Static load on supports, kg/cm² | 5.5 | ||
| Compressed air connection | ½” |
Fotogallery